Advanced Solutions in Waste Management: The HICLOVER Waste Incinerator
Introduction to HICLOVER Waste Incinerators
The waste incinerator produced by HICLOVER represents a critical advancement in waste management technology. Designed to meet rigorous industrial standards, these incinerators operate effectively within a temperature range that can reach up to 1200°C, ensuring the complete destruction of hazardous materials. With engineering reliability at the forefront, these systems are tailored to address the growing need for efficient waste disposal methods, particularly in regions where waste management infrastructure is lacking. The medical incinerator operating temperature standards established by relevant authorities are well adhered to, ensuring compliance with international safety norms.
Key Features of HICLOVER Waste Incinerators
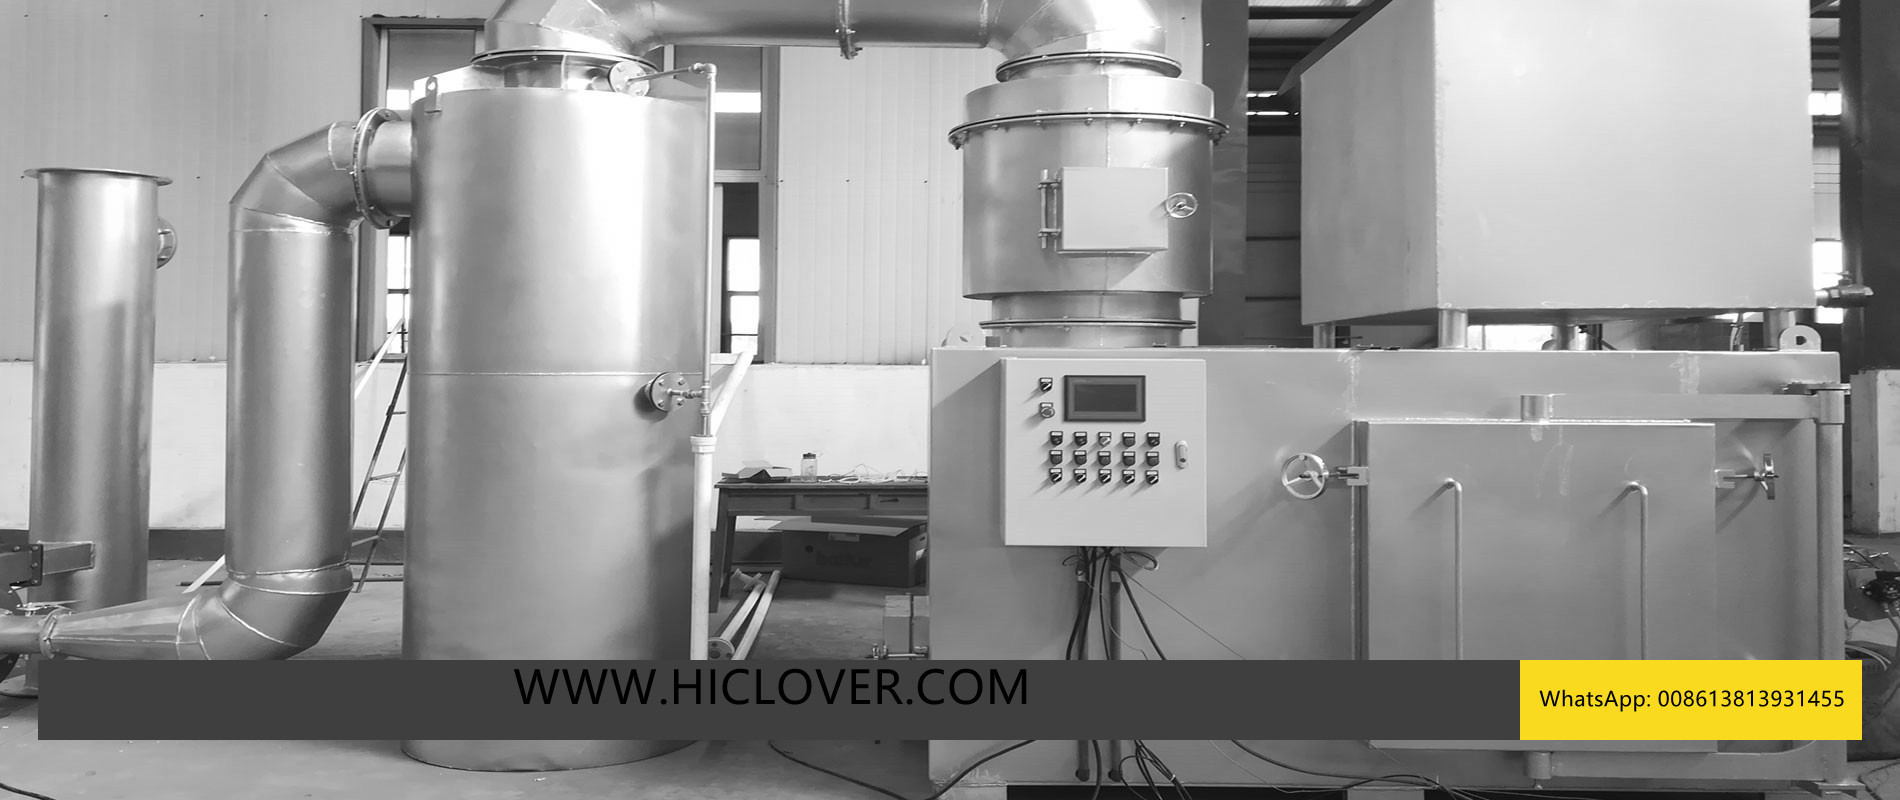
- Dual Chamber Combustion System: HICLOVER waste incinerators feature a dual combustion chamber design that enhances the efficiency of waste destruction. The primary chamber allows for initial waste combustion, while the secondary chamber ensures the complete oxidation of harmful gases, thus minimizing emissions and maximizing safety.
- High Temperature Retention: Maintaining a high temperature throughout the combustion process is vital. HICLOVER units are engineered to retain high temperatures consistently, effectively neutralizing hazardous materials and reducing the risk of dioxin formation.
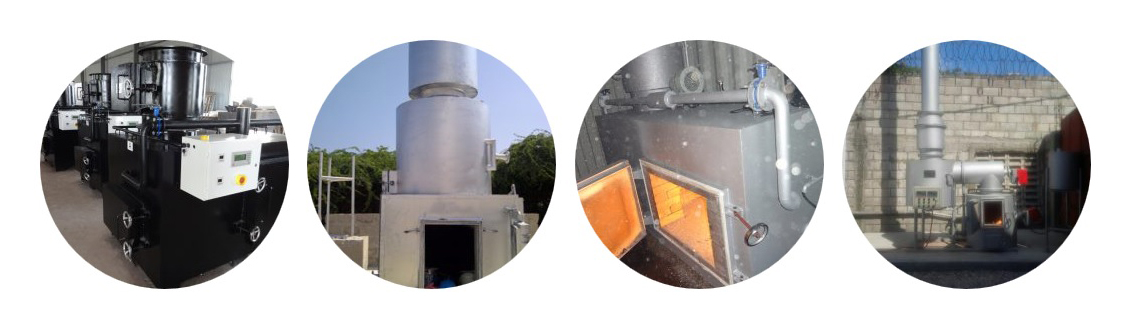
- Modular Containerized Systems: The containerized design of HICLOVER’s systems offers flexibility in deployment, enabling efficient installation in remote or crisis zones. This is especially useful for humanitarian camps and disaster recovery areas where waste needs to be managed swiftly.
- Multi-Fuel Capability: HICLOVER incinerators can operate on various fuels, including diesel, LPG, and natural gas, providing adaptability according to available resources.
- Remote Monitoring and PLC Control: Our systems are equipped with programmable logic controllers (PLC) for automated operation. This digital automation facilitates real-time monitoring and management, ensuring optimal performance and compliance with regulatory standards.
- Advanced Emission Control: The choice between wet and dry scrubbers allows users to select an emission control system that best fits their regulatory requirements. These scrubbers are essential for meeting the stringent emission standards enforced by authorities such as the WHO and EU.
Applications of HICLOVER Waste Incinerators
The versatility of HICLOVER waste incinerators allows them to be applied in various contexts:
- Medical Waste Management: Hospitals and clinics require reliable methods to dispose of infectious materials. HICLOVER’s portable medical waste incinerator is designed to handle such waste effectively, reducing the risk of contamination and ensuring compliance with health regulations.
- Animal Waste Disposal: In regions such as Ghana, where animal husbandry is prevalent, HICLOVER incinerators provide an efficient solution for managing animal waste. As a leading animal waste incinerator manufacturer, HICLOVER addresses the urgent need for biosecure waste disposal.
- Hazardous Waste Treatment: Countries like Uganda particularly benefit from HICLOVER’s systems, as they can incinerate hazardous materials that would otherwise pose significant environmental and health risks. The incinerators ensure safe disposal while adhering to international environmental standards.
- Emergency Response and Crisis Management: In times of crisis, such as natural disasters or outbreaks, the demand for waste incineration increases. HICLOVER’s mobile solutions can be deployed rapidly to manage waste in affected areas, maintaining public health and safety.
- Industrial Waste Processing: Industrial facilities generate large volumes of waste, and HICLOVER’s systems can be integrated into waste management plans, aiding in carbon emission reduction and operational efficiency.
Regulatory Compliance and Performance Standards
HICLOVER waste incinerators are built to comply with various regulatory frameworks. The systems are designed in accordance with international standards set by the World Health Organization (WHO) and the European Union’s emission directives, ensuring that emissions from these units are within permissible limits. The engineering team at HICLOVER continuously monitors technological advancements to stay ahead of regulatory changes, making our incinerators future-proof.
Key compliance standards include:
- Emission Limits: HICLOVER incinerators are tested against stringent emission limits for dioxins, furans, and particulates, ensuring safe combustion processes.
- Operational Efficiency: The dual chamber design enhances combustor performance, reducing the overall carbon footprint and aligning with current trends in carbon emission reduction pressure.
- Health and Safety Regulations: Ensuring the safety of operators and the surrounding community is paramount. HICLOVER’s designs incorporate fail-safes and monitoring systems that comply with health regulations.
Comparative Analysis of Incinerator Types
When selecting a waste incineration solution, understanding the differences between fixed and containerized systems is crucial.
- Fixed Incinerators: These are typically stationary and may require extensive infrastructure and permits. They are suitable for large-scale operations but can be costly to set up.
- Containerized Systems: HICLOVER’s containerized modular systems offer significant advantages. They are portable, require minimal site preparation, and can be operational in a fraction of the time compared to fixed installations.
In addition, HICLOVER’s waste incinerators can be operated manually or through PLC automation, providing flexibility based on user preference and operational needs.
Customizable Solutions for Diverse Needs
HICLOVER understands that different clients have varying needs. Our waste incinerators can be customized based on specific requirements:
- Chamber Volume: Depending on waste generation rates, clients can opt for different chamber sizes to optimize operational efficiency.
- Fuel Options: With the ability to run on multiple fuel types, our systems can adapt to local fuel availability, enhancing operational flexibility.
- Emission Control Options: The choice between wet and dry scrubbers allows for tailored solutions that meet local regulations and environmental compliance.
Supply Chain Stability and Engineering Expertise
HICLOVER’s strong factory manufacturing capabilities ensure a stable supply chain, critical for timely delivery and installation. Drawing from years of engineering experience, HICLOVER provides not only manufacturing but also technical support and maintenance services worldwide.
Our commitment to quality is evident in every unit produced. HICLOVER’s engineering team is dedicated to innovation, ensuring our waste incinerators are equipped with the latest technology, such as remote monitoring and automation features that enhance user control and efficiency.
For more information on our products, visit HICLOVER’s official website.
Conclusion
In the context of global infectious disease preparedness and crisis management, HICLOVER waste incinerators play a pivotal role in developing sustainable waste management solutions. As more regions like Mozambique and Uganda seek efficient waste management systems, HICLOVER continues to innovate, offering effective, reliable, and compliant waste incineration solutions. This commitment to quality and safety positions HICLOVER as a leader in the waste incineration industry, well-equipped to meet the challenges of today’s waste management landscape.